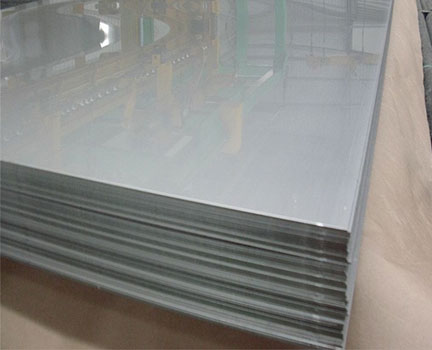
1. Chemical Composition
UNS S32205 / EN 1.4462 / ASTM A240, balanced dual-phase structure of approx. 50% austenite + 50% ferrite; typical chemical composition (wt%): C ≤0.03%, Cr:21.0~23.0%, Ni:4.5~6.5%, Mo:2.5~3.5%, N:0.14~0.20%, Fe balance.
2. Equivalent Grade under Different Standards
UNS: S32205
EN: 1.4462
ASTM: S32205 / F51
GB: 022Cr22Ni5Mo3N
JIS: SUS322J1
3. Production Process
3.1 Smelting & Continuous Casting
Raw materials are melted in EAF, refined via AOD plus VOD vacuum refining to precisely control Cr, Ni, Mo and nitrogen content for stable duplex microstructure. Continuous casting adopts electromagnetic stirring; all slabs are surface ground to remove subsurface cracks and inclusions.
3.2 Hot Rolled Coil Production (3.0–14mm, No.1 / pickled 2D finish)
Slabs are heated at 1100~1200℃, followed by rough rolling and finish rolling with finishing temperature above 900℃ to restrain harmful sigma phase precipitation. Critical solution treatment is performed at 1020~1100℃ with immediate water quenching; subsequent mixed acid pickling removes oxide scale to obtain hot rolled pickled feedstock coils.
3.3 Cold Rolled Coil Production (0.2–3.0mm, 2B finish)
Hot rolled pickled coils go through degreasing first, then multi-pass cold rolling on 20-high mill (single pass reduction ≤15% owing to severe work hardening). Continuous high-temperature solution annealing and rapid water quenching restore balanced dual-phase structure; followed by electrolytic pickling, passivation, skin-pass leveling, slitting and finished packaging.
4. Product Characteristics & Physical Properties
4.1 Mechanical Properties (annealed 2B condition)
Yield strength Rp0.2 ≥450MPa, Tensile strength Rm ≥620MPa, Elongation ≥25%, Hardness HB ≤290. Yield strength is nearly twice that of 316L austenitic stainless steel, enabling lightweight design under equal pressure load.
4.2 Physical Features
●Excellent chloride corrosion resistance with PREN ≥34; outstanding resistance to pitting, crevice corrosion and chloride stress corrosion cracking, far superior to 316L for seawater and high-salt environments.
●Moderate thermal conductivity and lower thermal expansion coefficient than austenitic grades, resulting in less thermal & welding deformation.
●Fine low-temperature toughness and outstanding fatigue resistance; acceptable weldability by GTAW/GMAW/SAW with proper welding procedure.
●Cost-efficient alternative to high-alloy super austenitic stainless steel such as 904L.
5. Main Applications
●Marine & Desalination Industry: Seawater heat exchangers, reverse osmosis equipment, offshore platform pipelines, marine pump & valve components, ship ballast tank lining.
●Petroleum & Petrochemical Industry: Sour oil & gas transmission pipelines, refinery desulfurization towers, acid reaction vessel liners, chemical storage tanks compliant with NACE anti-sulfur specification.
●Environmental Protection: Power plant FGD flue pipes, waste incineration tail gas facilities, high-salinity wastewater treatment tanks and piping.
●Pulp, Food & Pharmaceutical Industry: Pulp bleaching equipment, food fermentation tanks, sanitary process piping for beverage and pharmaceutical production.
●New Energy & Construction: High-pressure vessels, LNG auxiliary parts, coastal anti-corrosion decorative profiles and heat exchanger coils.