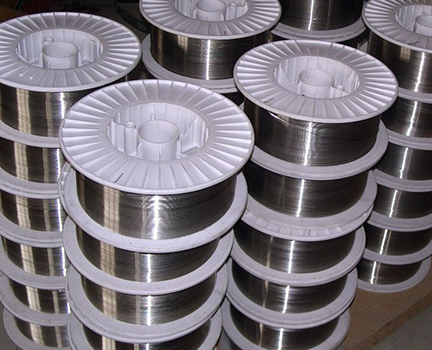
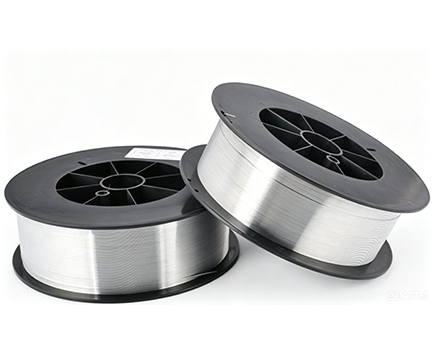
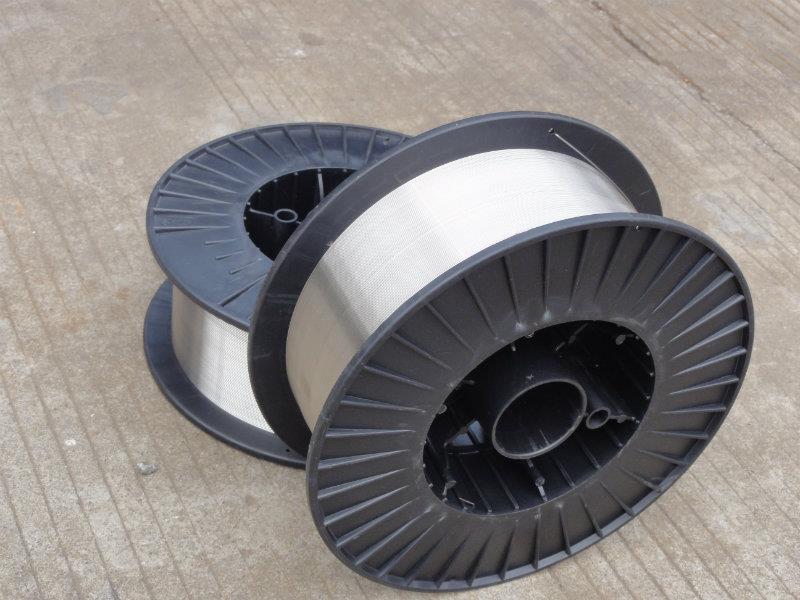
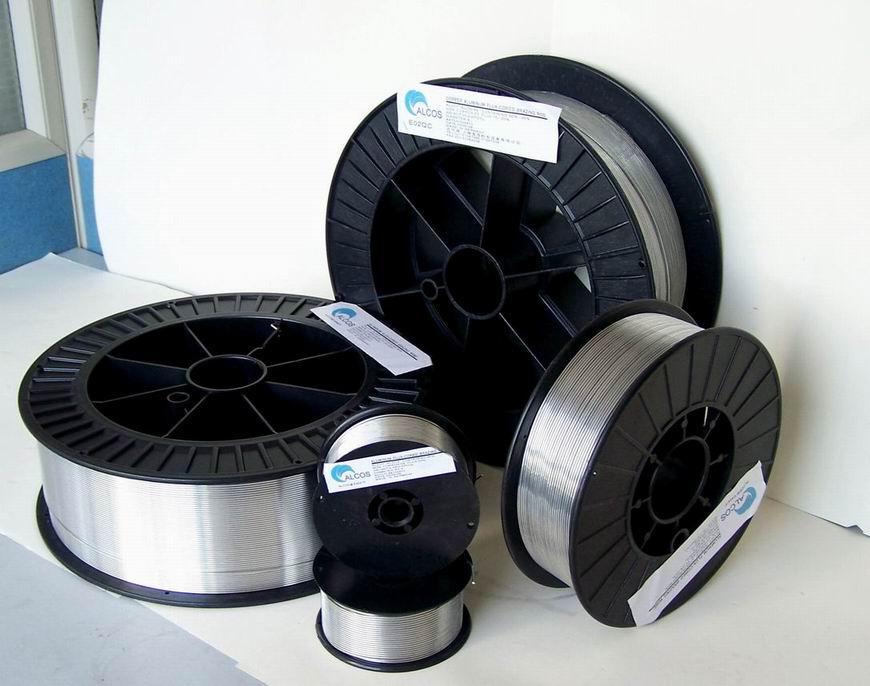
ER308 Gas-Shielded Solid Wire
Widely used in petrochemical, pressure vessel, food machinery, medical equipment, fertilizer equipment, textile machinery, nuclear reactor, etc., such as welding of 12Cr18Ni9 (SUS 302), 06Cr19Ni10 (SUS 304) and other materials.
Welding Wire Chemical Composition(Wt%)
| AWS | Welding wire chemical composition(Wt%) | |||||||||
| C | Mn | Si | Cr | Ni | Mo | P | S | Cu | Other | |
| ER308 | 0.035 | 1.8 | 0.31 | 20.15 | 9.52 | 0.03 | 0.013 | 0.008 | 0.34 | – |
Product Welding Reference Current(AC Or DC+)
| Wire diameter(mm) | ¢0.8 | ¢1.0 | ¢1.2 | |
| Welding current(A) | Flat welding, horizontal welding | 70-150 | 100-200 | 140-220 |
| vertical welding | 50-120 | 80-150 | 120-180 | |
| Overhead welding | 50-120 | 80-150 | 160-200 | |
NOTE:
- Shield gas: Must ensure not to operate with impurity shield Gas.Recommendation Rate of mixed gas: Ar+1-3%O2.
- Operation flow rate of shield gas: 20-25L/min.
- Electrode extension: 15-25mm
- The welding should be operated in clean surface without rust, moist, oil contamination and dust.
- Prevent affected of wind when wind speed reach 1.5m/s to avoid bubbles generated.
The above suggestions are for reference purpose. Evaluate and determine the situation of the scene before starting the wielding process.